 Courtesy Irons Brothers
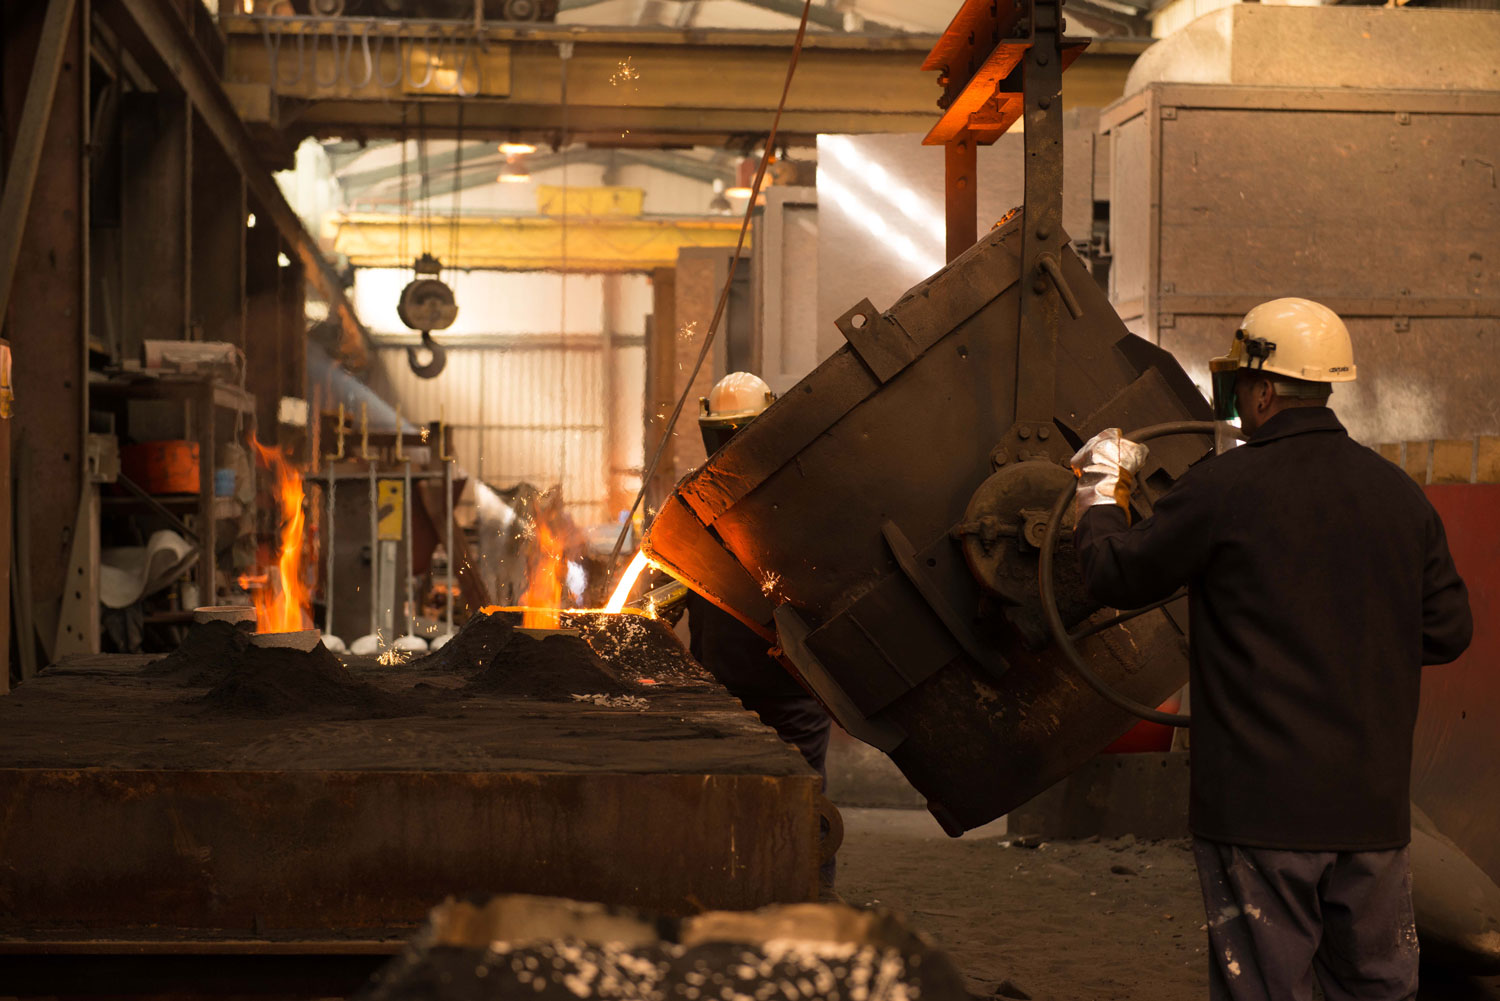
The shop fills with the snap of sparks at Irons Brothers foundry (Cornwall, U.K.) as iron heated to over 1,320°C (2,408°F) flows along a channel to a giant ladle, which will then pour it into waiting molds.
The 77m (252.6′) superyacht M5 (ex-Mirabella V) has several claims to fame. When launched in 2003, she was the biggest single-masted sailing yacht in the world, and her 291′ 11″ (89m) carbon fiber mast was the tallest ever built. Her 20,450-square-foot (1,900m2) reacher was the biggest sail in the world—the size of three soccer pitches. Everything about her, from the two cinemas to the 29′ (8.8m) custom-built Hinckley tender, was excessive.
Less well known was the boat’s 150-tonne (165.3 ton) lift keel, which extended her draft from 12′ 10″ (3.9m) to 33′ (10m). Made from fabricated steel filled with lead, it was later modified and fitted with a sacrificial tip weighing about 30 tons, in case of collision with an underwater object. When the boat struck a whale off Chile, the sacrificial tip duly sheared off and sank, protecting the boat from worse damage. A new tip was cast and shipped out to America where it was fitted to the keel by divers. The boat remained in the water.
 Jay Panetta
The foundry specializes in yacht keels of all shapes and sizes, including this complex recent job delivered to Rockport Marine (Rockport, Maine) comprising a lead bulb fitted to a steel fin section that serves double-duty as a 2,000-liter (528.3-gallon) fuel tank.
The source of the original keel and the two sacrificial lead bulbs was the Irons Brothers foundry, located well off the beaten track in Cornwall, U.K. Founded exactly 100 years ago this year, the company diversified into yachting in the late 1960s and has supplied keels for virtually all the major European production boatbuilders, from Westerly to Bénéteau to Oyster. It has also made keels for some of the top racing yachts in the world, including several TP52s and Open 60s. Alex Thomson of Hugo Boss fame is a repeat client. More recently, it has provided a complex two-part keel for the 95′ (28.9m) Project Ouzel being built by Rockport Marine in Maine.
I visited the foundry earlier this year to find out what makes the company so, well, hot. The town of Wadebridge sits at the top of the Camel estuary on the north coast of Cornwall. It’s better known as a foodie hub—Rick Stein has a restaurant in nearby Padstow, and Gordon Ramsay lives in nearby Rock—than a center of boatbuilding excellence. The most famous boatbuilder in these parts was Cornish Crabbers, which was based in Rock and Wadebridge, before it went into liquidation last year.
 Courtesy Irons Brothers
Set in the Cornish countryside, Irons Brothers occupies a 5.5-acre (2.2-hectare) industrial site.
The foundry is located down an idyllic leafy lane, a mile out of Wadebridge. As I parked next to the old stone building where the offices are located, I imagined a rustic workshop, with an open fire and pots of molten metal poured by grubby-faced craftsmen. The reality is that Irons Brothers is a huge operation spread out on a 5.5-acre (2.2-hectare) site, with two furnaces (one for iron and one for lead), a machine shop, a pattern shop, and various finishing rooms. The main shed alone is 300′ (91.4m) long. In short, it’s a serious commercial venture, rather than a quaint cottage industry.
 Nic Compton
Irons Brothers chairman, Matthew Robinson, right, with managing director Nigel Burt.
From One Tonners to Foilers
Matthew Robinson, current chairman, and managing director Nigel Burt, told me how it all started in 1925, when three brothers, William Edison, Joseph Leonard, and Ernest Clifford Irons (all known by their middle names) bought out the existing forge for £350 (US$1,690 in 1925). Like George Harris before them, the Irons Brothers continued to supply pumps and other equipment for the local china clay industry before they fell out and Edison and Leonard went their own way, leaving Clifford to run the company on his own.
Clifford’s son Henry, who took over the company in the 1960s, had an interest in yachting and made the first foray into what was then a burgeoning market: a one-tonne keel cast for Kelly & Herbert boatbuilders, on the south coast of Devon. Soon after, he established a connection with Marine Projects in Plymouth, who built Moody Yachts, and Westerly Marine in Hampshire, who built their own range of sailing yachts. Once those contacts were made, it seems, the work never stopped coming.
“Henry got in right at the beginning, when production boats for pleasure had just started,” says Robinson (Henry’s son-in-law). “He made keels for the young Rob Humphries and Tony Castro—we still deal with them both today.”
Yacht keels quickly became the company’s main business, with orders coming in from Rustler Yachts, Southerly, Parkers, Westerly, Sadlers, Rival Bowman, and Spirit Yachts. “We made every keel that Oyster put on a boat, which must be well into the hundreds,” says Burt (Henry’s nephew). In fact, Oyster Yachts’ website puts the company’s total sales at more than 1,100 boats.
 Courtesy Irons Brothers
Despite a recent downturn in yacht sales, Irons Brothers still builds between 500 and 700 keels every year, many for production builders.
Inevitably, Irons Brothers has seen some client boatyards close (Westerly, Sadler, and Bowman, to name but three), often owing the foundry large sums of money, none of which they’ve ever managed to recover. Yet somehow, they have survived. While 90% of U.K. foundries have closed in the face of cheaper competition from abroad, Irons Brothers has remained the foundry of choice for Europe’s boatbuilders. Even now, with new boat sales flattening out across most of Europe, the company still produces around 500-700 keels per year while employing 27 people.
“It’s a niche market,” says Robinson. “It’s often about making a small number of things, but you need big equipment to make them. We can pour a lot of metal, and we can move heavy things arounds. Lots of other foundries can do that, but they are generally 1,000 times bigger than we are, and they’re not interested in making a single keel for an Oyster 885—they want to make 1,000 things. The boatbuilding industry also requires much tighter casting tolerances than most foundries are geared up for. We are used to that, and to the finish expected on an Oyster.”
About 45% of the company’s current business is export, mostly to Europe, including Elan, Nautor Swan, Hallberg-Rassy, Bénéteau, Dufour, Jeanneau, and smaller companies such as Black Pepper in France. American production boatbuilders are a smaller market, though the company used to supply ballast to Luhrs in Florida back in the 1980s, and they still work on many bespoke projects in the U.S. The recent keel for Rockport Marine was one of the more complex orders they’ve had to deal with, being made of two parts: a lead bulb and a fabricated steel section, which doubles as a fuel tank, with the associated plumbing inside. The idea is to free up space inside the boat, as well as putting the weight of that 2,000 liters (528.3 gallons) of fuel as low as possible in the hull.
 Nic Compton
Freshly cast lead keel bulbs shine after initial sandblasting and fairing.
Irons Brothers remains very involved in yacht racing, and each Vendée Globe race will invariably see several of their bulbs cantering around the world at improbable speeds. Even modern foiling boats need ballast, not just for their canting keels, but for the foils themselves. “We’ve made loads of tiny, intricately shaped lead pieces which are set into various parts of the structure, wherever they are needed,” says Burt. “They are a bit weird and wonderful.” At the other end of the industry, the company also supplies plain lead ingots for internal ballast to powerboat companies such as Princess, which might need to alter a boat’s trim. Curiously, all lead ingots are still made in the traditional 26kg (57.3 lbs) size, even though EU guidelines stipulate that 25kg (55.1lbs) is the maximum weight one person can safely carry on their own.
Shop Tour
Robinson showed me the factory, starting with the two fabrication shops opposite the office and then on to the foundry itself. It’s a fascinating window into the process of keel-casting and some little-known details of local history. The building which houses the offices, for instance, used to be three worker’s cottages. Edison Irons was born in one of them, while another has a hole in the floor where a coffin was carried out. Before the foundry existed, explosives were made on this site for use in Cornwall’s tin and copper mining industries—including inventing a safety fuse that was encased in lead to prevent it from being set off accidentally. A conveniently overhanging branch on a large oak tree in the yard was used as a crane to load products onto carts.
As we walk around the foundry, it’s clear that on top of the history, this is very much a thriving modern operation. There are keels in various stages of manufacture for a whole host of well-known companies and boat models. A cast-iron top section for a Nautor Swan 51 keel awaits its lead bulb, while a lead bulb for a Swan 58 performance keel stands idle as its cast-iron fin section is off to the Midlands to be CNC machined for absolute precision. There’s half of a keel for a Six-Meter designed to be removable so the owner can load the boat onto a trailer. That’s on a truck heading to Barcelona. Elsewhere, there are cast-iron fins and bulbs for Hallberg-Rassy, Jeanneau, and X-Yachts, while outside a line of nine keels, finished and painted, awaits collection. Robinson has a quick look and confirms they are destined for Bénéteau and Elan.
 Nic Compton
Wooden patterns, the basis for any casting, are kept in a storage shed at the foundry.
Keel making most commonly starts with a wooden pattern made in-house using drawings printed onto Mylar. (Irons Brothers has experimented with CNC pattern making but found the old-fashioned Mylar templates work better.) Those patterns are intentionally slightly oversize to allow for shrinkage when the metal cools—0.5% for lead and 0.8% for iron. The company is contractually obligated to keep the keel patterns for as long as the boats are in production; in practice, it tries to keep as many as possible for as long as possible—in case a replacement is needed. Consequently, there’s a huge shed full of old patterns, some dating back 50 years. It’s a remarkable service to the general boat owner or service yard who can ring up and order a keel for, say, a Westerly Centaur, and the chances are good they will still have it and can cast a new keel without having to charge to make a new pattern.
Once the pattern is finished, it is used to make the mold in one of the hundreds of hefty steel boxes stacked up around the foundry. A mixture of sand and resin is poured into each half of the box, and the pattern is used to create an impression of the desired shape. The exact mix of hardener to resin varies depending on the task at hand, with less hardener usually used for the bigger jobs to allow more working time. Once the sand mixture is set, the pattern is removed, and the inside of the mold is coated with a clay-based liquid that acts as a release agent.
 Nic Compton
Steel boxes filled with sand and resin imprinted with the shape from a pattern serves as a mold for casting.
For boats with a big production run, they sometimes make a metal mold (called a chill), which can be reused many times to manufacture lead keels, although this is much more expensive.
Irons Brothers cast iron and lead keels; the differences between the two are significant. Iron weighs 7,200kg per cubic meter (449.5lb/ ft3), compared to 11,300kg per cubic meter (705.4lb/ft3) for lead. The cost of the scrap metal used to make iron keels, however, is just £300 ($404) per ton, compared to £2,300 ($3,095) (at time of writing) for lead. Despite this, the company’s production ratio has shifted from twice as many iron keels in the past, to slightly more lead keels now.
“Lead is superior because it doesn’t rust, and it’s very dense, so a smaller area of keel has more weight,” says Robinson. “Most production boatbuilders use cast-iron keels because they are so much cheaper. But there are more millionaires than ever now, and boats are getting bigger and bigger. Our average casting has gone up from 1 tonne (1.1 tons) to 2.5-3 tonnes (2.7-3.3 tons).”
Unfortunately, neither of the furnaces was in action when I visited the yard, but Robinson showed me the enormous cupola, the steel bucket in which the iron is melted. The company uses recycled car brake disks—guaranteed Grade 17 iron—to make cast-iron keels. And, indeed, just around the corner from the cupola was a huge pile of them, waiting to be melted down. There was also a large heap of coke—imported from Poland since the U.K.’s last coal mine closed down in 2008—which not only supplies the heat to melt the iron but also give it its carbon content.
 Nic Compton
A shoal of recycled car brake disks will be melted down to be reborn as cast-iron keels.
The car disks and coke along with some limestone and other ingredients are all loaded via a belt into the cupola, which is then fired up and heated to over 1,320°C (2,408°F) for the iron to melt. Once the metal is flowing and the ingredients are mixed, a clay plug at the bottom of the cupola is removed allowing the molten metal to run along a channel to a ladle, which is then carried to the waiting boxes where the iron is poured into the molds. About 40 tonnes (44.1 tons) of iron is melted at a time—enough for about 15 keels. The metal stays liquid for about 20 minutes, though this can be extended by covering the ladle with insulation.
I noticed the floor around the iron furnace was covered in a deep layer of sand. Matthew explained that if any molten iron was spilt and hit a concrete floor, it could cause an explosion due to the potential moisture content of concrete. The sand insulates the floor and contains any stray liquid metal, preventing it from spreading.
By comparison, casting lead is simple. Although it’s possible to recycle lead from a variety of sources, Irons Brothers only use lead bought as ingots from a trusted refiner in Derbyshire. This ensures the metal is of a guaranteed quality, with a precise amount of antimony mixed in—usually 3%—to impart the right degree of stiffness in the final cast part. Even when old lead keels they have made in the past are offered to them for recycling, they will only use them to make ingots for internal ballast, where no structural strength is required. The chance of using an impure batch of lead is simply not worth the risk when people’s lives are dependent on the keel not dropping off in a storm halfway across an ocean.
 Courtesy Irons Brothers
Pouring molten iron in excess of 1,320 °C (2,408 °F) into a mold. The metal remains in liquid form for about 20 minutes.
Once the lead is sourced, it’s simply a matter of chucking it into the smaller furnace—in 23-tonne (25.3-ton) batches this time—and heating it to 320°C (608°F) using an oil-powered centrifugal burner. The molten lead is channelled into a ladle and poured into the molds as before. Unlike cast-iron keels, where the bolt holes are bored and threaded after the metal has cooled, lead keels are often poured with a steel bolt matrix carefully placed in the keel mold. The other option is to drill plain holes for through bolts after the metal has cooled, as the metal is too soft to be threaded.
 Courtesy Irons Brothers
Prior to pouring, the mold for a lead keel is fitted with a grid of steel to support the keel bolts that will attach the appendage to the hull.
Although simpler to make, lead keels are harder to estimate costs of than cast-iron ones. Lead and antimony are a traded commodities on the London Metal Exchange (LME), so prices fluctuate from day to day. China controls about 50% of the world’s antimony (used to make bullets and nuclear weapons as well as keels), and in December 2024, China banned export of the critical mineral to the U.S., quadrupling its price in the space of a few months. That means a quote for a lead keel has a time limit, and if a customer is slow to order, the company has to run the figures again using the latest LME prices. The world of high finance meets the world of low ballast.
Once the metal has set, the casting boxes are opened and the keels removed, sand blasted to remove any debris, then faired and painted. This is a dangerous process for lead keels as the dust is toxic. They are cleaned up in a sealed workshop, with workers wearing full PPE and filtered breathing apparatus. Staff who work on lead keels have a blood test every six months to check they are not being contaminated. In 25 years, only one person has recorded high levels of lead, and they were immediately moved to another department.
Irons Brothers also takes on repair work, and in one workshop I visited, a lead keel was being excavated to remove the old bolt matrix and fit a new one. Fresh lead would then be poured into the cavity to fix the new bolt material in place before the keel is sent back for reinstallation.
 Nic Compton
Repair work includes projects like replacing the internal bolt structure in an otherwise serviceable old lead keel.
Beyond Keels
Cannons have long been an important sideline at the foundry, providing an unexpected link to the days when explosives were made on the site. Anyone who has been to Valetta in Malta in recent years will have heard the 32-pounder cannons Irons Brothers cast firing twice a day—likewise, for cannons in Oman, the Tower of London, Guernsey, and the Bermuda Maritime Museum. As a result, the company holds a firearms license and benefits from regular visits from the London Proof House (“home of gun proof since 1637”) to check the durability of their products. “When the Maltese cannons were being proofed, the explosion was so loud that it set off car alarms in the Co-Op car park in Wadebridge, which is a mile away,” says Robinson. “Some of the boys were standing 120m (394′) away, and they said it was like being hit on the chest with a spade.”
When I visited the foundry, two freshly cast aluminium wheels were cooling off on the side, looking very much like outsize parts from an Airfix model kit, with their runners (channels for the incoming metal) and risers (for the overflow) still attached. They were part of a machine made in Cornwall that sifts out precious nuggets from piles of slag in gold and other heavy metal mines around the world. As these precious metals rise in value, it has become worthwhile to extract the small nuggets that were previously ignored. It’s also a direct link back to the Cornish mining industry that Irons Brothers itself was founded on.
Other weird and wonderful work that the company takes on includes waterwheels, shepherd’s hut wheels, banjo tone rings, artist’s sculptures, and cast-iron road signs known as fingerposts. Once upon a time, Robinson tells me, there were four foundries making fingerposts in Cornwall, each in a slightly different style. Some of them included an image of a hand pointing in the direction of whatever town or place was being signposted. One foundry took it a stage further and took a mold from the pointing hand of the head foreman’s son, ensuring the child’s posterity for the next 200 years.
 Nic Compton
Irons Brothers thrives on a diversity of casting projects from keel to wheels to canons to signposts.
The scale and scope of the operation requires numerous skills from pattern-making to fabrication (they even make the wooden carriages for many of the cannons they supply), to casting, blasting, and finishing. The work is at once brutal and potentially explosive (that molten iron) and yet intricate and delicate (those bronze wings, cast and bolted to some Six-Meter keels). It requires a rare combination of brawn and sensitivity not to mention some sharp business acumen to keep on top of the financial markets.
It would take a huge investment to create this foundry from scratch, and yet the returns are relatively modest in pure business terms. Irons Brothers works and excels at what it does because it is a family business that has been going for 100 years and doesn’t have any investors or shareholders breathing down its neck. It has unparalleled knowledge and experience of the business, a skilled workforce, and no debt.
“If someone had £2m to invest, I wouldn’t recommend they bought a foundry!” says Robinson. Yet he and Burt clearly derive enormous satisfaction from continuing a business that has been in the family for a century, creating a product that gives pleasure to thousands and is eminently recyclable. Or, as Robinson puts it: “It’s nice to know something you’ve made is sailing around somewhere.”
About the Author: Nic Compton is a freelance writer/photographer based in Devon, U.K. He lived on boats in the Mediterranean until the age of 15 and worked as a boatbuilder for many years before swapping his chisel for a pen and his router for a computer. He sails a Rhode Island–built Freedom 33, currently based in Greece.