 Nicole Jacques
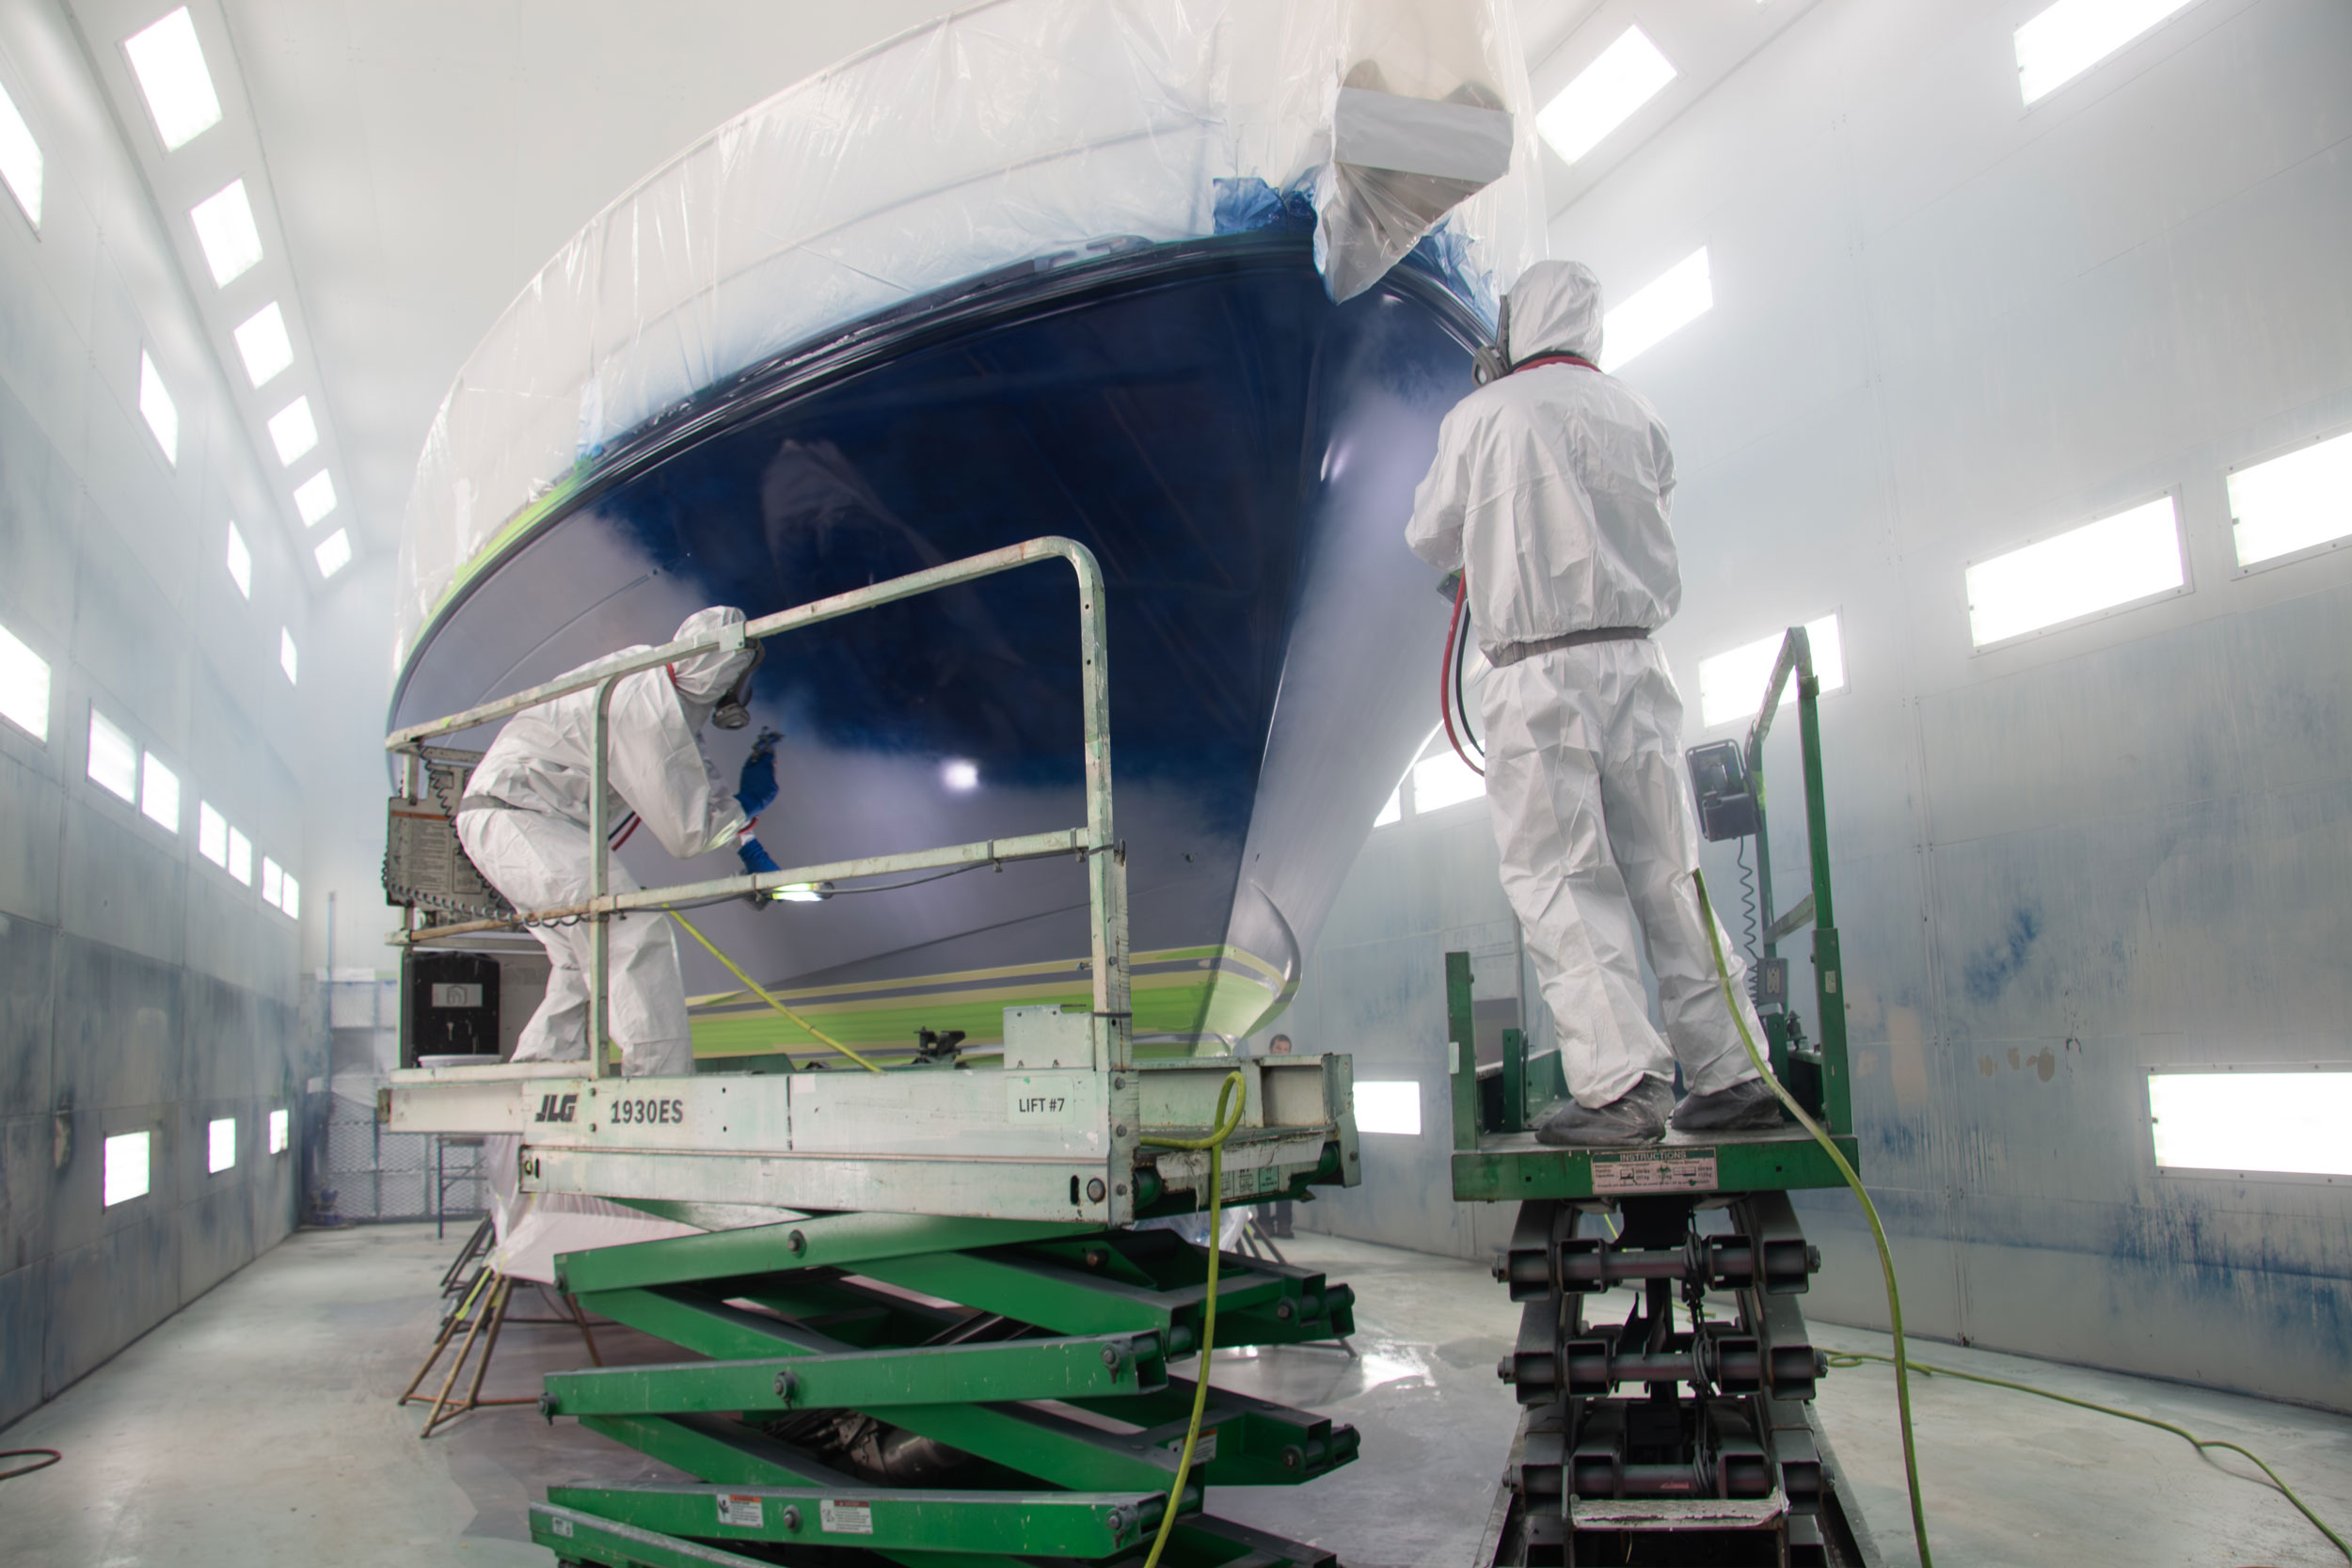
After hours of work preparing the hull surface as well as the paint itself, technicians spray topcoat on a boat at Front Street Shipyard in Belfast, Maine.
The afternoon before the first coat of topside paint went on a 100’ (30.5m) sloop, the crew of applicators at Front Street Shipyard in Belfast, Maine, gathered to talk through the spray plan. They prepped their tools, surveyed the plastic tenting, and documented the products to be used. Thirteen containers of an off-the-shelf shade of red acrylic paint were stacked inside the tent; the hull would take roughly six gallons per coat, with two full coats planned. As the painters pried open the first cans, anticipation turned to alarm. The shades of red inside were wildly different—some deep and muted, others shockingly bright. Despite the identical labels, it was clear: These were not the same color.
If the painters had sprayed straight from the cans, the result would have been a splotchy, tie-dyed mess on the hull. The color variations were far too extreme to produce a uniform finish. Fortunately, this veteran crew had seen it before, which is exactly why they opened all the cans before loading a single one into the spray gun. Their resourceful solution is called “boxing”—pouring all 13 gallons into one oversized tub, mixing thoroughly until the hue evens out, then redistributing the blended paint back into the cans. Now, every tin held the same bright crimson tone the owner had envisioned. They could start the first spray.
Boxing isn’t a new technique, but its necessity—as well as other methods to manage variations in topside coatings—is becoming increasingly part of the equation for boatyards and other professionals working for customers who expect a flawless finish. Evolving paint formulations, changes in chemistry, extended cure times, fine-print warranties—all require applicators to plan, document, and manage a paint job well beyond the technical skills needed to apply paint itself. Learning how to respond effectively to a paint chemistry landscape that is constantly changing, often without warning, is arguably the hardest part of the job.
 Front Street Shipyard
Before boxing, four can lids from the same red paint show slight and dramatic color differences. Other variations can include viscosity, gloss, and tone.
The seasoned pro who led the sloop’s paint team was Juan Carlos España of Peake Coating, a Virginia-based coatings application company that brings skilled painters into boatyards along the East Coast for short-term, subcontracted projects, usually for high-value yachts. España has painted hundreds of boats throughout his 30-plus-year career, ranging from tenders to superyachts. Over the decades, he’s learned and developed countless adaptations to application methods that improve his own efficiency and project outcomes, especially as the chemical makeup of paints has evolved over the years.
Generally, a paint technician starts the boxing process by shaking and opening every container of paint. Before mixing anything, he works his way down the row of lids, dragging a stir stick through the paint that’s collected on each one. In the same way a sommelier might read the legs on a wine glass, a technician can read the paint—its tone, viscosity, and gloss—and subtle differences often jump out immediately. A greenish cast in one lid among several blue hues is enough to prompt a closer look.
When a can looks too far off, he may pull it from the lineup before it ever reaches the mix. Only after every container passes inspection does he combine the paint into a single batch, ensuring one uniform, predictable coating before the gun ever comes out.
 Bill Robishaw
Several gallons of midnight blue paint are opened and ready to be boxed.
España started incorporating the boxing technique into all his coatings work more than 15 years ago as metallic paints were rising in popularity. Achieving a consistent metallic flake density across the entire surface of the hull required evenly premixing all the cans of paint and flakes together in a single vat before application. España quickly realized boxing would defend against other potential inconsistencies beyond flake density, so it became a standard practice in his coatings process. Working across nearly every major marine urethane system, he boxes all paint products—acrylics and polyesters alike—regardless of manufacturer.
For him, boxing is as much about risk management as craftsmanship. By uncovering as many challenges with the paint’s color, viscosity, and composition as he can before a spray gun is ever loaded, he reduces his own exposure. It’s España’s commitment to protecting his hard-won professional reputation that drives his attention to detail and record keeping. If the finished paintwork fails, he believes the customer will hold him responsible—even in instances when the cause traces back to the paint’s chemistry.
“In my experience, an unhappy customer will never point his finger at the paint maker,” España says. “He’ll blame it on the boatyard.” Consistency isn’t an issue with just one brand, so España declines to nitpick specific products. “All paint brands come with their own quirks,” he says. His growing concern, however, is the increasing frequency of color inconsistencies in cans he opens across boatyards nationwide. What were once occasional anomalies have become routine, and he feels he has no recourse with the manufacturers.
“Either you warranty your product or you don’t,” España says of the paint vendors. “When I read a paint label that says, ‘color variation is possible,’ it seems like there’s no guarantee. How can I use that product on an expensive yacht?”
 Nicole Jacques
When boxing paint, applicators combine and mix all cans for a spray job ahead of time to even out any variations.
Reading the Technical Data Sheet (TDS) for any modern paint can be surprising. España points to one TDS that now warns against buffing and polishing for “certain color shades,” although no specific hues are identified. Explaining to an owner fresh off a major repaint that the finish can no longer be buffed or polished is an unrealistic message to deliver. Carefully reviewing the TDS for every paint product each time it’s used is essential, because the manufacturer’s information can change between batches.
Control What You Can
To head off paint problems that increasingly feel inevitable, boatyards have started shouldering more overhead in time, cost, and liability. Forward-thinking managers may even be recognizing the need to raise paint pricing to reflect the expanded preventive measures that applicators like España now consider essential. Boxing paint is only the beginning; exhaustive documentation, prolonged curing, and extended sourcing timelines have become standard. Some of these efforts stave off potential problems, while others are simply to establish some recourse when things still go wrong.
The best preventative measure is keeping time-coded and dated records that provide a comprehensive account of environmental conditions, including ambient, surface, and material temperatures; humidity and dew points; and airflow management. Critical documentation also includes all materials used from the first day of hull or deck preparation through final topcoat application, repair compounds, high-build primers, inks, and sandpaper grits. Every paint container’s data—particularly batch numbers and expiration dates—are included. The guiding principle: No detail is too small.
Since España is usually on the road without a conventional office, he keeps a handwritten journal for each job. His phone’s photo roll is also filled with time-stamped shots of every project in each stage of the prep and paint process from all angles. España frequently teams up with Bill Robishaw, paint department manager at Safe Harbor Front Street (formerly Front Street Shipyard), for major projects. On those jobs, documentation is effectively doubled, with Robishaw keeping his own comprehensive coatings report as a spreadsheet saved to his computer. When issues arise during a spray, the first move is to compare notes. A systemic problem should reveal itself in the documentation, although given the number of variables involved, pinpointing the source is seldom straightforward. When the documentation affirms that every protocol has been followed to the letter, the paint product itself becomes the likely suspect.
Robishaw also maintains the same detailed records on test panels, which have become an increasingly important tool for catching potential issues before the actual spray. Regardless of the marine paint system he’s applying—most commonly acrylic or polyester, with enamel used by rare request—test panels offer an early indication of how the coating will lay down and its expected cure time. Even if it’s a product he uses frequently under controlled paint-booth conditions, he doesn’t feel confident the paint from one batch will behave the same as paint from another since product inconsistencies have become so common. One issue he frequently detects on test panels is variation in cure times, which he feels could be a possible harbinger of deeper problems.
 Nicole Jacques
At Front Street Shipyard, an applicator sprays individual boat parts, which offers an opportunity to test paint color and behavior before shooting a complete hull or house structure.
“Cure times for some products are getting a lot longer than they used to be,” Robishaw says. “We sometimes even need to apply additional heat to speed it up.” Reluctant to rely on the cure time stated in a product’s TDS—some of which now extend to three weeks—he sets up his own science experiment inside the paint bay to verify the completed cure. Using a test panel sprayed alongside the boat’s topsides, he applies and removes masking tape each morning following the application to determine more precisely when the paint is real-world ready for additional detailing, such as a cove stripe or pinstripe. He notes that acrylic coatings have long required at least twice the cure time of polyester, and that those cure windows now appear to be extending even further.
Longer cure times that keep boats in the paint bay are only part of what’s slowing paint schedules overall. Applicators face a growing list of time-consuming steps to ensure the best possible finish, starting with where to buy the material. For his most exacting customers, Robishaw says one way he reduces the risk of inconsistency is by cutting out the middlemen in the supply chain. Factory-direct paints tend to offer greater consistency than those mixed and delivered by distributors. Most brands are willing to facilitate factory-direct purchases upon request, but delivery times usually increase significantly.
The longest delays occur when every preventative step fails and the finish develops discoloration, dust, sags, or adhesion problems that demand a full rework. Sanding off the coating and re-prepping the surface for another spray consumes several days and dozens of labor hours. Then the coatings team reviews the documentation, makes adjustments to the product or process, and sprays again.
Regardless of whether the failure originates with the material or the method, customers aren’t willing to pay extra for anyone’s mistake. And few boatyards have the time, leverage, or resources to challenge a paint manufacturer. The result is almost always the same: The cost of a re-shoot falls squarely on the boatyard, turning the project into a financial loss.
“No one estimates a job to do things twice,” says Robishaw.
 Nicole Jacques
Days of prep work, including precise taping of bootstripes and meticulous hull sanding and priming, is critical to a paint job’s positive outcome.
Best case, an applicator catches a problem as it emerges early in the spray and then adjusts tools, materials, or environmental conditions before proceeding. Experienced applicators rely on powerful, handheld LED flashlights to read the surface in real time. With a spray gun in one hand and the light in the other, they watch how the paint lays down against the hull or deck, looking for anything out of the ordinary. Robishaw explains that a polyester urethane should hit the surface already resembling the finished product. When the reflected light on the area shows a clean, uniform gloss, it’s time to move the gun to the next area. Acrylic urethanes behave differently, appearing first as fine beads that gradually flow together as they cure—a characteristic that makes them slightly more forgiving during application. Any anomaly in the paint’s behavior during the spray should immediately raise a red flag.
Some warning signs get missed. Robishaw recalls a hard-won lesson from a paint job on a RIB several years ago managed by a colleague. With three coats planned, the crew prepped the hull, boxed the paint, documented every step, and started spraying. Near the end of the third coat, they ran out of material, leaving them with no other option except to open a new container of paint labeled as the same color. As the hull cured, the port bow quarter dried to a noticeably different shade. The only remedy was to sand the hull and start over. Since then, Robishaw has intentionally overestimated material quantities, ensuring an extra gallon or two of paint is available for touch-ups or repairs down the line.
Having a leftover gallon of boxed paint can be a lifesaver for owners. The odds are high that a boat will eventually brush a dock or worse and require a touch-up or localized repair. Some owners take a spare gallon with them when they leave, but many prefer not to store chemicals aboard or at home, opting instead to leave the paint with the yard.
Robishaw sees this as part of his responsibility to help customers maintain their finishes, so his shop houses rows of chemical cabinets filled with paint—clearly labeled with each vessel’s name—reserved for those inevitable repairs. That service, however, comes at a cost: valuable space in an already crowded boatyard.
“Ever since we started boxing, storage has become an issue,” explains Robishaw. “Now we have to buy more chemical cabinets to store it all, even though we don’t currently charge for paint storage.”
 Front Street Shipyard
A miscalculation in needed paint quantity led to slight variations in the gray topcoat on this RIB.
In most cases where a spare gallon isn’t available, a repair relies on the boatyard’s paint technician to color-match the existing finish. Even with records of the original paint formula, applicators can no longer expect a perfect match from the manufacturer, given the growing inconsistency in color. Whether the applicator requests a color match from the factory or uses toners to dial it in by hand, the application process is critical to achieving a seamless blend. Every experienced technician develops personalized methods for achieving the best possible result. Robishaw relies on a specific blending solvent during repairs, which he feels produces excellent results with urethane paints.
“I have my method, and other people have tricks like putting excessive reducer in their final coat of a repair to make it easier to blend,” he says. “None of it is perfect.”
Some paint pros turn to a spectrophotometer to help match existing colors. Used in all types of color matching from boats to cars to walls, a digital spectrophotometer is a handheld electronic device that shines a light onto a color sample and then measures the wavelengths of light reflected back. The device then translates wavelength data into a numerical value the paint technician can use to establish a color mixing formula. When assessing how well a sample color matches the boat’s existing color, a digital spectrophotometer can produce a second, critical metric called the Delta E, which quantifies the color difference between the hull and the repair. A paint technician will work to get the Delta E as close to zero as possible.
Quest for Consistency
Boatyards are doing more and more to work around paint inconsistencies, but those fixes aren’t free, and the costs are often getting absorbed by the business, shaving down already thin margins. At some point, the industry has to ask whether these problems should be solved in the paint bay or, instead, at the factory.
Some degree of inconsistency is unavoidable, according to Chris Toole, product manager at Hempel UK Ltd. and a certified coatings inspector with the Association for Materials Protection and Performance. Toole has quite literally written the book on the subject as a co-author of “Paint Colour Guide: Yacht Coating Technical Guidelines,” a white paper published by the International Council of Marine Industry Associations. His advice to boatyards echoes what España and Robishaw emphasize: Work with reputable suppliers that maintain rigorous quality controls, box paints before application, and retain spare material for future repairs. These precautions are essential, not necessarily because problems are likely, but because minor variations are inevitable.
A paint technician confronting these issues day after day might reasonably question whether today’s coatings are falling short of expectations. But it’s important to distinguish between a standard and a tolerance. Take Flag Blue, for example. The color is assigned a numerical value within a manufacturer’s color system, and that value represents the standard reading on a spectrophotometer. Each batch, however, is produced within an allowable (Delta E) tolerance around that standard. Those allowable tolerances vary by manufacturer. As a result, two paints from the same brand labeled the same color can still differ subtly, even when both technically meet specification.
 Nicole Jacques
Three samples of one paint brand’s Flag Blue reveal color variations. Paint manufacturers face challenges when regulations for pigments essential to the color formula change.
When asked how modern paint formulas are affecting color consistency, Toole reframes the question: “It is more accurate to ask, ‘How [are] regulation and health and safety affecting the quality and consistency of applications?’ ” Toole explains that in an effort to maintain uniformity, manufacturers typically rely on single-source suppliers for raw materials. When international regulations governing those materials change, or when their supply chain availability is disrupted, manufacturers are often forced to reformulate, introducing variables that can affect consistency from batch to batch.
“It is fair to say that most of these changes are negatively affecting the quality,” Toole acknowledges.
By way of example, Toole points to blue pigments that have been heavily regulated due to their chemical composition. As those materials were restricted, manufacturers were forced to adopt alternative, more naturally derived substitutes, which simply weren’t as vibrant. Carbon black has also experienced periods of limited availability, affecting a wide range of colors. Titanium dioxide faced similar pressure; it was under regulatory scrutiny for years and at one point appeared likely to be banned, a disastrous scenario given its widespread use in white paints. Although that legislation was ultimately overturned, Toole recalls titanium dioxide shortages several years ago created many of the same challenges as an outright ban.
“At one point,” says Toole, “I believe one major paint company either purchased, or was about to purchase, their own titanium dioxide plant.”
Toole offers some reassurance that most consistency issues such as color variation or extended cure times are unlikely to compromise a product’s overall performance. Longer curing, for example, may be inconvenient, but it’s typically a function of the coating’s chemistry, mix ratios, temperature, and other application variables, rather than a symptom of product failure.
“If quality is measured by the in-service performance, then it can be the quality of the formulation, raw materials, substrate prep, and other factors that will define ‘quality,’ but not the cure time.”
Some paint technicians—and even distributors—believe manufacturers should be more transparent about formulation changes when a supply-chain issue requires a chemical modification. Every time factories adjust formulations, those changed products arrive at boatyards without notice or explanation on the label. A product delivered today may differ significantly from one with the same label received just weeks earlier—something experienced applicators notice immediately. Compounding the issue, many warranties exclude coverage unless a long list of specific conditions is met.
Tim Walenga, technical sales representative at Midwest Industrial Coatings Inc., says the steady drip of small, undocumented changes is eroding trust between brands and their users.
“How about making sure I have a good product on the front end, so I don’t need a warranty later?” he asks.
Walenga has spent 38 years in the paint industry, witnessing the evolution from single-stage coatings to intermix systems and, ultimately, to today’s two-part polyester and acrylic paints. He currently mixes and distributes products from four major marine paint brands, along with liquid, powder, and electrodeposition coatings for agricultural and industrial markets. He has strong confidence in his operation, where batches of up to 250 gallons are blended in a single vat, an approach that helps ensure consistent color from can to can. Smaller mixing facilities around the country, by contrast, may only be able to blend five gallons at a time, increasing the likelihood that paints shipped to boatyards will show noticeable color variation and require boxing.
In his role, Walenga hears frustrations from both sides of the equation, boatyards and manufacturers alike. He tries to convey his customers’ concerns to the brands, hoping they’ll take concrete steps to improve consistency. Still, he doesn’t anticipate any sweeping changes to paint chemistry in the near term.
“I wouldn’t say there will be a huge reformulation anytime soon,” he says. “I just see the big companies getting feedback from their customers to make what they have better.”
Those customers are hopeful that manufacturers are listening. Back at Safe Harbor Front Street, Robishaw has begun steering owners away from products he once favored. Acrylics, which he long recommended for their ease of application and long-term repairability, no longer perform as they once did—an observation echoed throughout the industry, according to Walenga. Despite carrying the same labels, applicators are finding today’s acrylics far more difficult to repair, effectively eliminating the very advantage that made them a go-to choice.
“When a manufacturer changes their product, we find out the hard way through application,” Robishaw explains. “If we then decide we don’t like the new chemical makeup of a brand that we’ve been using for a while, we need to find another product to fill that void.”
Across the country, applicators increasingly feel that products they once trusted have become high-stakes experiments on very expensive boats. And if, as Walenga suggests, there is no breakthrough chemistry on the horizon to replace what once worked reliably, the industry’s path forward lies in improving the consistency of the products already in use. Paint technicians aren’t asking for miracles—they’re asking for transparency when formulas change, meaningful technical support when problems arise, and warranties that acknowledge the realities of today’s application environment.
About the Author: Nicole Jacques is a communications professional with more than 20 years of experience helping boatyards and marine businesses tell their stories. She serves on the board of the American Boat Builders & Repairers Association and is an active sailor and industry advocate.


